The mold determines your production capacity, block quality, and profitability for years. Yet most new manufacturers choose based on initial price rather than production requirements, leading to costly replacements and capacity limits.
Mold selection affects production volume, product range, and operational costs for 5-8 years—the typical mold lifespan. This guide provides the technical framework manufacturers use to specify molds matching their machine capabilities and market requirements.
Understanding Block Machine Mold Fundamentals
What Cavity Count Actually Means
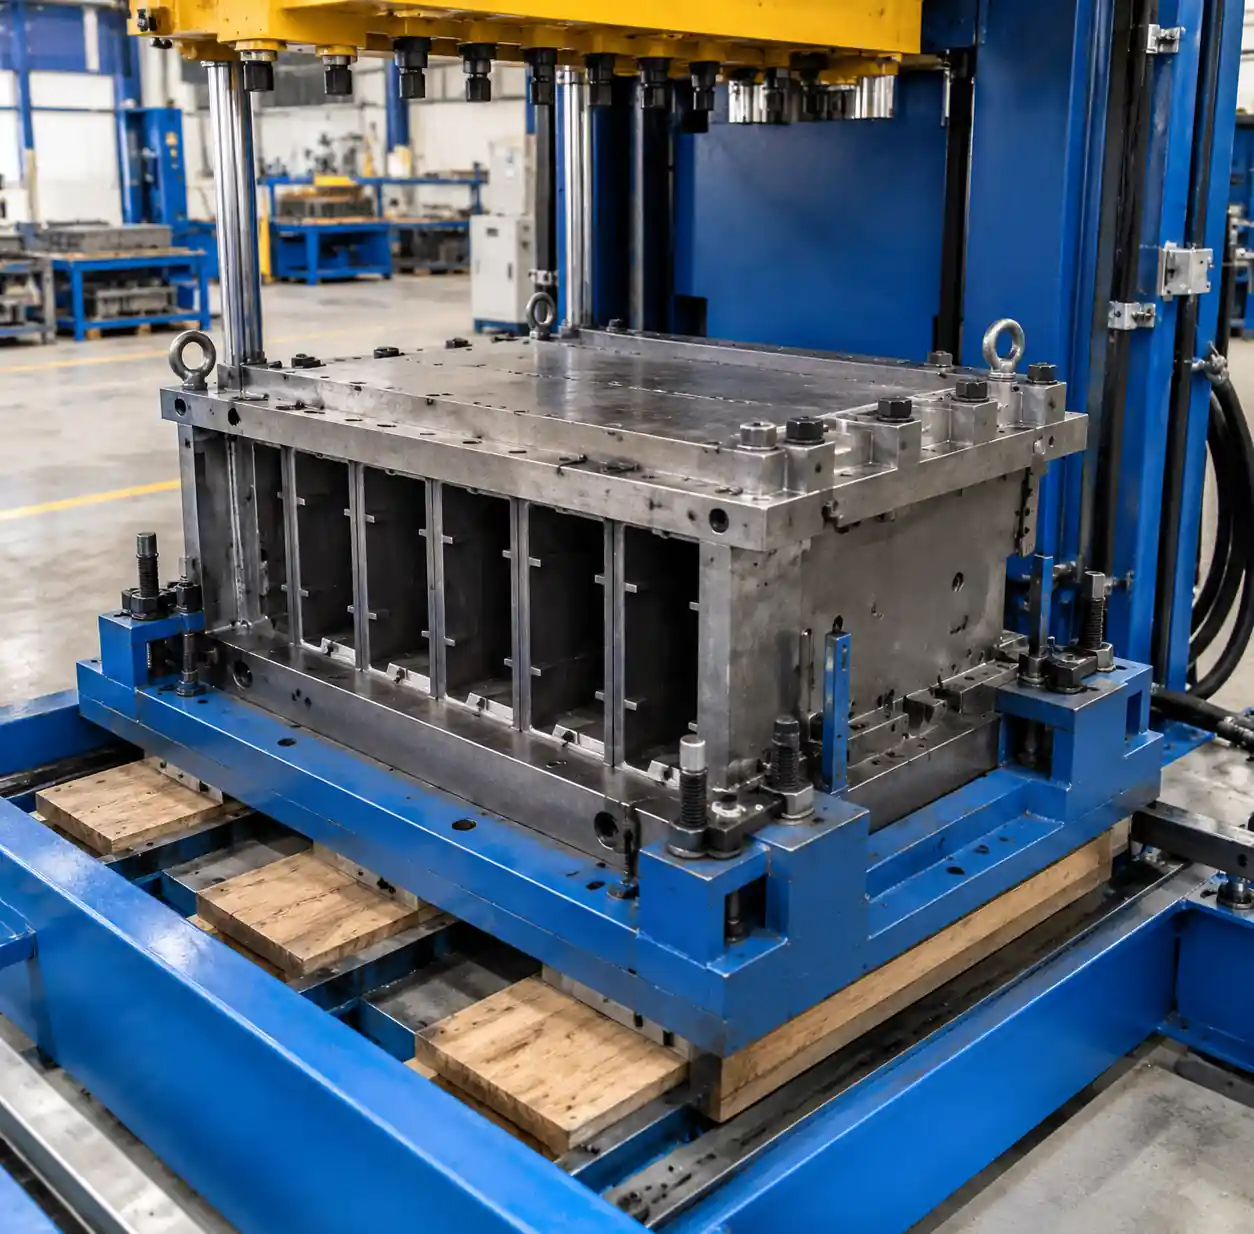
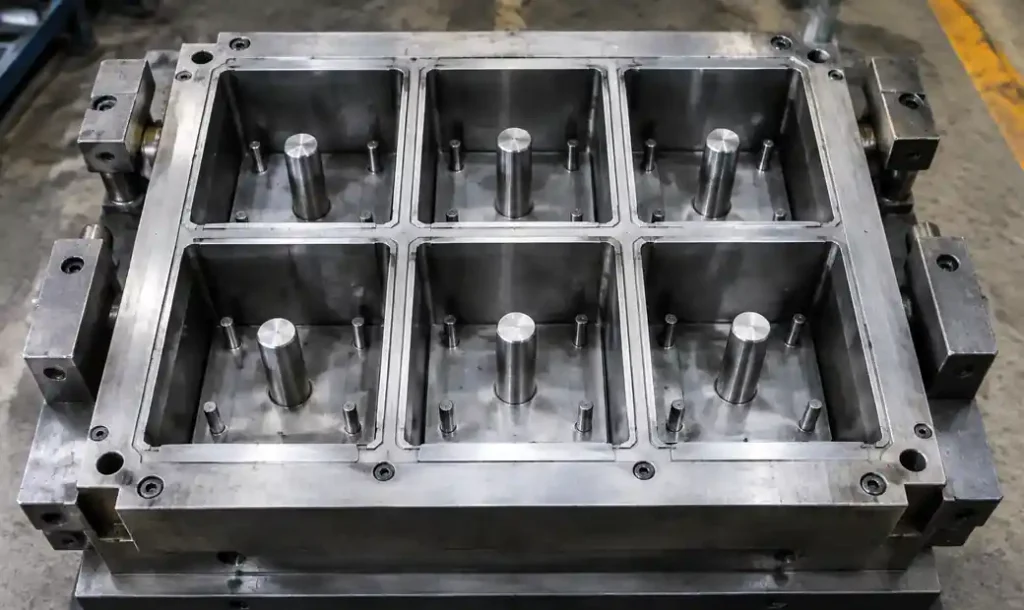
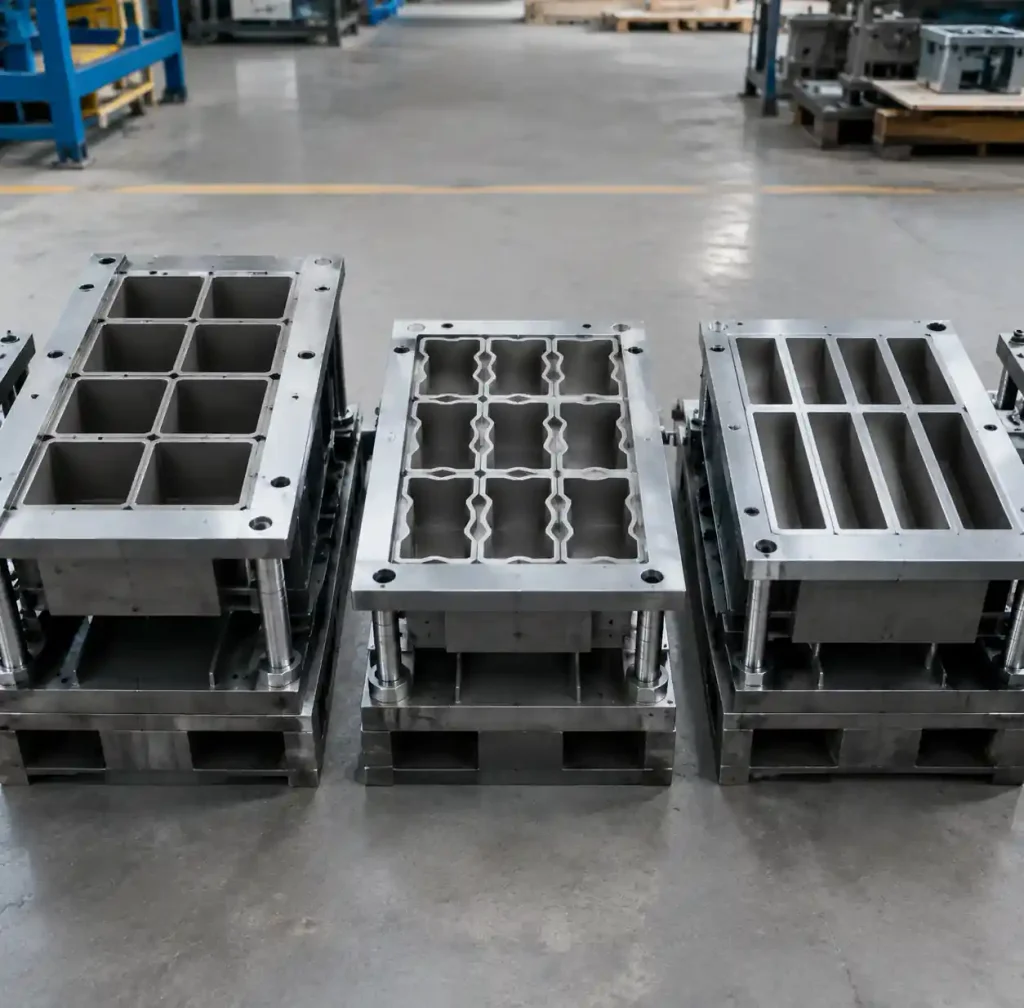
Cavity count is the number of block impressions filling simultaneously in one cycle. A 4-cavity mold produces 4 blocks per cycle, directly multiplying capacity.
The formula: Daily output = cavities × cycles/hour × hours × efficiency. A semi-automatic machine at 15 cycles/hour, 8 hours, 85% efficiency with 4 cavities produces 408 blocks daily. Upgrading to 6 cavities increases output to 612 blocks—50% more from the mold alone.
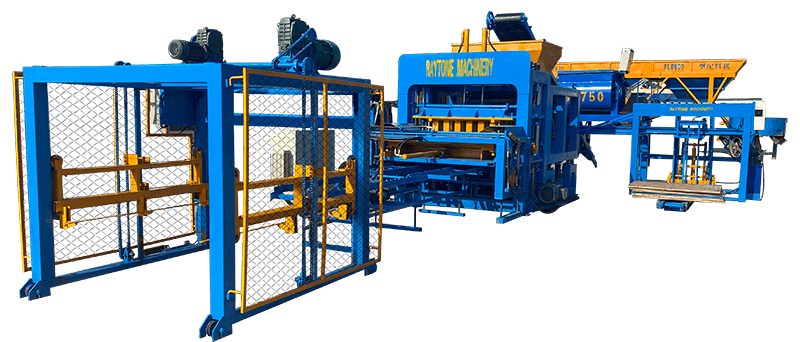
Machine limits exist. A آلة قطع يدوية with 150 kN force handles 4 cavities maximum for 400×200×200mm blocks. Automatic machines with 400-600 kN accommodate 6-10 cavities depending on block size.
Mold Materials and Their Performance Characteristics
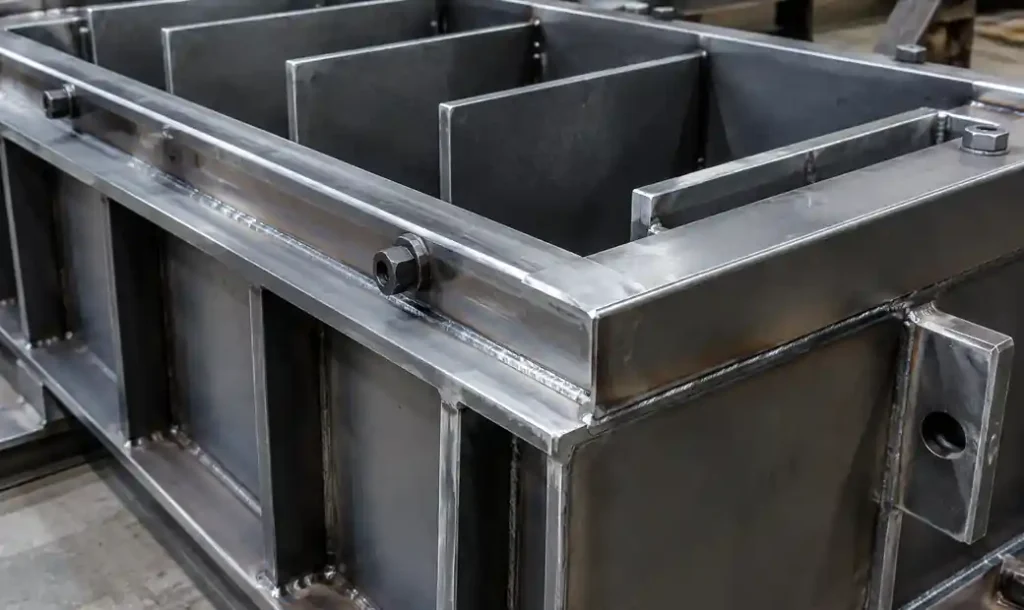
Steel molds: Fabricated from Q235 or Q345 structural steel for standard use, upgraded to 45# carbon steel or alloy steel (40Cr, 42CrMo) for high-wear applications. Steel molds deliver 50,000-100,000 cycles with proper maintenance and maintain ±1.5mm tolerances.
Advantages: Superior durability, dimensional stability, weldable for repairs, handles high forces. Limitations: Heavier (120-350kg), requires anti-corrosion treatment, higher cost ($800-$3,500).
Hardened inserts: Critical surfaces—cavity corners, core pins, ejectors—use hardened tool steel (HRC 55-60) welded into standard frames. This extends life 60-80% while controlling costs. High-volume producers (100,000+ blocks monthly) should specify hardened inserts for molds exceeding 80,000 annual cycles.
Cavity Configuration Selection Matrix
| Production Target | Manual Machine (12-15 cycles/hr) | Semi-Automatic (15-20 cycles/hr) | Automatic (20-30 cycles/hr) | Recommended Cavity Count |
|---|---|---|---|---|
| Small-scale (<5,000 blocks/day) | 3,000-4,500 blocks | 4,500-6,500 blocks | 6,500-10,000 blocks | 3-4 cavities |
| Medium-scale (5,000-15,000 blocks/day) | Limited capacity | 7,500-12,000 blocks | 10,000-18,000 blocks | 4-6 cavities |
| Large-scale (15,000-30,000 blocks/day) | Not suitable | Not suitable | 18,000-35,000 blocks | 6-10 cavities |
| High-volume (>30,000 blocks/day) | Not suitable | Not suitable | 35,000-50,000+ blocks | 8-12 cavities |
Operating efficiency assumes 85% for manual systems, 88% for semi-automatic, and 92% for fully automatic lines. Single-shift (8 hours) is standard; multiply by 1.9 for double shifts accounting for maintenance.
Block Type and Design Complexity
Standard Hollow Blocks
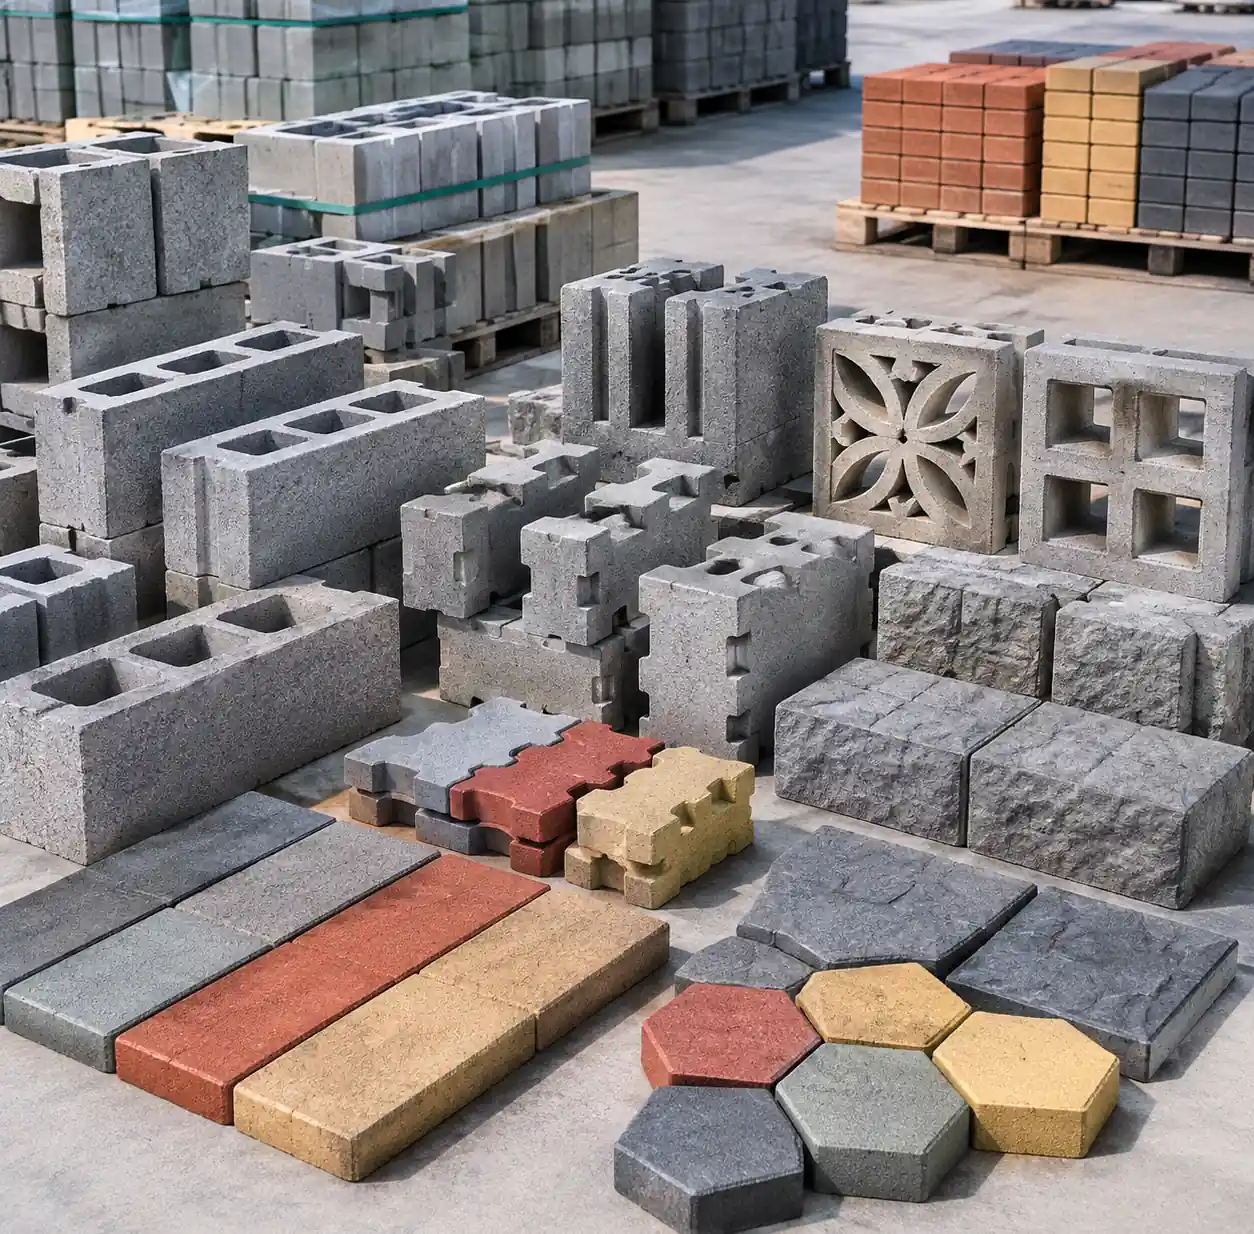
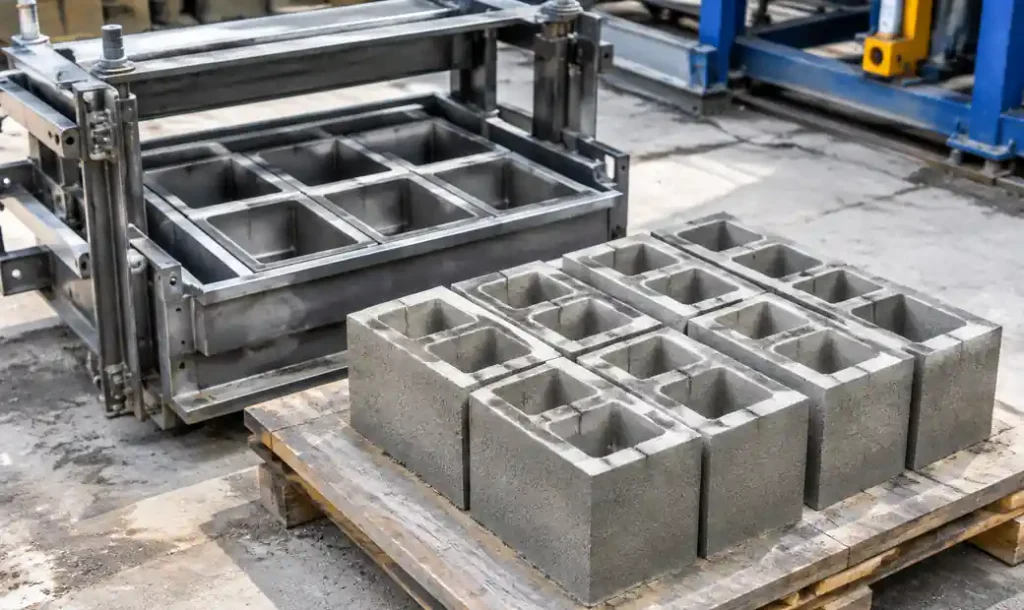
Standard hollow blocks (400×200×200mm, 390×190×190mm) with 2-3 rectangular cores represent baseline complexity. A 300 kN machine handles 6 cavities of standard hollow blocks comfortably.
Core configuration affects compaction. Rectangular cores aligned with vibration direction compact more uniformly than circular cores. Core walls should maintain 25-30mm minimum—thinner walls crack during demolding.
Interlocking and Specialty Blocks
Interlocking blocks require precision tolerances (±0.5mm) reducing cavity count by 30-40%. A machine producing 6 standard cavities typically handles only 4 interlocking cavities due to force requirements and dimensional control.
Specialty shapes—curved blocks, decorative faces, ventilation blocks—increase cycle times 15-25% from extended vibration and careful demolding. Factor these into capacity calculations.
Paver Blocks
Paver production uses different logic. Pavers are thinner (60-100mm) but need high surface quality and precision. Paver molds typically have 8-20 cavities depending on size.
Textured surfaces, color layers, and patterns reduce cavity count and increase cycle time. A smooth 200×100×60mm paver mold accommodates 15 cavities, while interlocking or patterned versions produce only 10 cavities.
Material Selection for Production Environment
Standard Carbon Steel (Q235/Q345)
Suitable for moderate volumes (<60,000 blocks/month), standard designs, covered operations, and budget-conscious buyers.
Service life: 50,000-70,000 cycles with maintenance. Maintenance: Weekly cleaning, monthly inspection, annual anti-corrosion coating. Cost: $800-$2,000 for 4-6 cavity hollow block molds.
Alloy Steel (40Cr, 42CrMo)
Suitable for high volumes (>80,000 blocks/month), complex designs with thin walls, outdoor operations, and long-term ROI focus.
Service life: 100,000-150,000 cycles. Maintenance: Same cleaning as carbon steel, superior dimensional stability. Cost: $1,800-$4,500 for 4-6 cavities—2.2-2.5× carbon steel cost but 2× life delivers 10-15% lower cost per block.
Hardened Inserts (Selective Reinforcement)
Producers exceeding 100,000 blocks monthly should consider selective hardening. Hardened inserts (HRC 55-60) protect high-wear areas: cavity corners, core pins, ejector plates.
This delivers 70-80% of alloy steel durability at 40-50% cost. Carbon steel with hardened inserts costs $1,400-$2,800 and achieves 85,000-110,000 cycles versus 50,000-70,000 for standard steel.
Custom Mold Design Process
When Standard Molds Don’t Fit
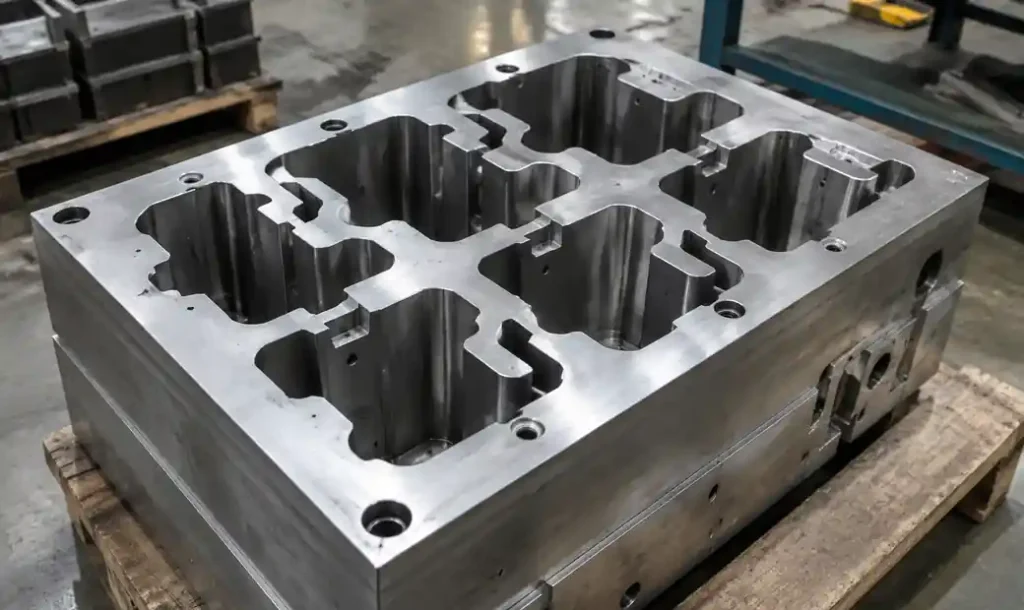
Standard molds accommodate 80% of demand: hollow blocks (2-3 cores), solid blocks, basic pavers. Regional preferences, specialized applications, or competitive differentiation often require custom designs commanding 20-40% price premiums.
Technical Specifications Required
Manufacturers need precise specifications to quote custom molds:
- Block dimensions: Length, width, height with tolerances (±2mm structural, ±1mm architectural)
- Core configuration: Number, size, position, and geometry of voids
- Surface requirements: Smooth, textured, embossed, or color interfaces
- Production volume: Annual quantity determines material selection
- Machine specs: Model, pallet dimensions, maximum force, vibration frequency
Providing CAD drawings (DWG or STEP) accelerates quoting and eliminates errors. Include cross-sections showing internal geometry.
Timeline and Investment
Lead times: 4-6 weeks for simple designs, 6-10 weeks for complex geometry, 10-14 weeks for specialized designs requiring prototyping.
Investment ranges $2,500-$8,000 depending on complexity, cavity count, and material versus $800-$2,500 for standard molds.
Custom molds make economic sense when product commands ≥20% premium, annual production exceeds 200,000 blocks, or customer contracts specify unique geometry.
Mold Compatibility with Machine Types
| نوع الآلة | Platform Size | Force Range | Vibration Type | Optimal Cavity Count | Mold Weight Limit |
|---|---|---|---|---|---|
| Manual | 850×550mm | 100-180 kN | Manual/pneumatic | 2-4 cavities | 80-150kg |
| Semi-Automatic | 850×550mm to 1,050×680mm | 200-350 kN | Electric vibration | 4-6 cavities | 150-280kg |
| Fully Automatic | 1,050×680mm to 1,200×800mm | 400-600 kN | Electric dual-axis | 6-12 cavities | 280-450kg |
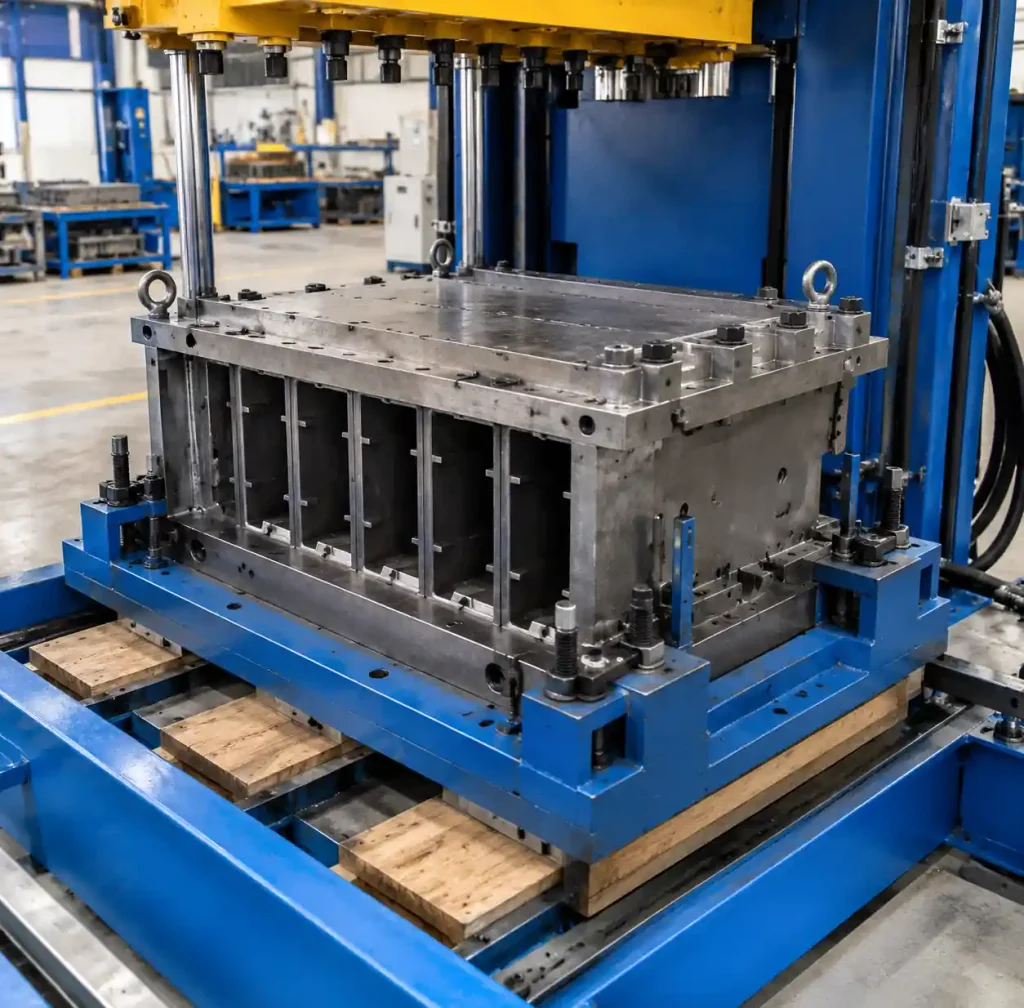
Platform dimensions constrain physical mold size. A semi-automatic machine with 850×550mm platform cannot accommodate larger molds regardless of cavity configuration. Calculate mold dimensions including frame thickness (80-120mm) to verify fit.
Pressing force determines cavity capacity. Each 400×200×200mm hollow block requires 50-65 kN for proper compaction at 160-180 bar. A 300 kN machine handles 4-5 cavities (allowing 10-15% margin). Exceeding force capacity produces weak blocks with inconsistent density.
Mold Maintenance and Longevity
Daily Maintenance
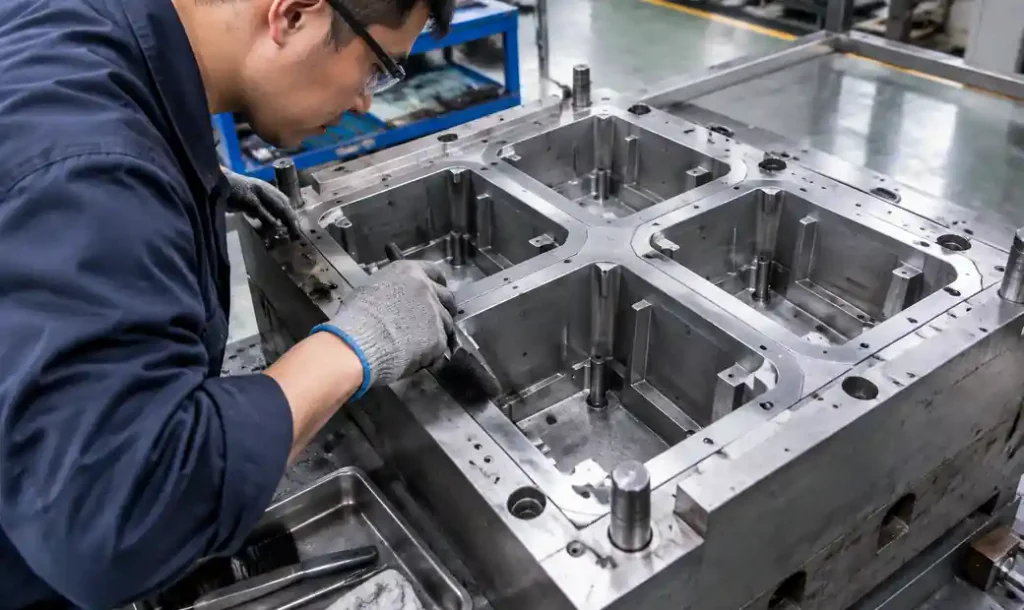
Clean molds thoroughly after production removing all concrete residue. Buildup creates surface defects and increases demolding force by 15-25%, accelerating wear. Use proper release agents—never petroleum-based products.
Inspect for damage: hairline cracks (at weld joints), surface scoring, bent core pins, loose fasteners. Early repairs cost $50-$150 versus $800-$2,500 for complete replacement.
Dimensional Verification
Measure critical dimensions monthly using precision calipers. Track dimensional drift—progressive changes indicate wear requiring intervention. Blocks maintaining ±2mm tolerances are acceptable. Dimensions beyond ±3mm produce blocks rejected by quality-conscious customers or failing standards (ASTM C90, BS EN 771-3).
Interlocking or precision architectural blocks require weekly measurement. Interlocking tabs wearing ±0.5mm prevent proper block fit.
Refurbishment vs Replacement
Molds at 40,000-60,000 cycles typically need refurbishment: welding worn areas, replacing core pins, remachining surfaces. Refurbishment costs 35-50% of new price and extends life 20,000-35,000 cycles.
Replace molds when frame distortion exceeds ±3mm, wear is widespread (refurbishment approaches 60-70% of replacement), design becomes obsolete, or upgrading cavity count for expansion.
Economic Analysis: Cavity Count and ROI
Capacity vs Investment Trade-offs
Higher cavity counts deliver proportional capacity increases but investment doesn’t scale linearly. Comparing 4-cavity vs 6-cavity for standard hollow blocks:
4-cavity: $1,200-$1,800 investment. Daily capacity ~480 blocks (semi-automatic, 8hrs). Production cost $0.042-$0.048/block.
6-cavity: $1,600-$2,400 investment (+$400-$600). Daily capacity ~720 blocks (+50%). Production cost $0.038-$0.043/block (-$0.004-$0.005/block).
The 6-cavity mold costs 33% more but reduces per-block cost 8-10% while increasing capacity 50%. Break-even occurs at 80,000-120,000 blocks depending on selling price. Producers exceeding 200,000 blocks annually should prioritize capacity over initial cost.
Multi-Mold Strategies
Successful manufacturers invest in 2-3 specialized molds: 1) High-volume standard hollow blocks (6-8 cavities), 2) Solid blocks or alternate sizes (4-6 cavities), 3) Premium products—interlocking, pavers, architectural (lower cavity count, higher precision).
Mold changeover on automatic machines requires 15-25 minutes. Two runs daily (morning standard, afternoon specialty) provides flexibility while maintaining efficiency. Schedule minimum 3,000-5,000 blocks per mold to amortize changeover time.
Regional Considerations and Standards
International Block Standards
ASTM C90 (North America): Specifies minimum face shell thickness 25mm, web thickness 25mm, compressive strength 13.1 MPa for hollow load-bearing units. Molds must produce these dimensions accounting for ±2mm tolerance and minor shrinkage.
BS EN 771-3 (Europe): Defines dimensional tolerances ±3mm for length/width, ±2mm for height, and strength classes 2.9-20+ MPa. European markets require tighter dimensional control than ASTM applications.
Regional preferences: Middle East favors larger formats (400×200×300mm, 500×200×200mm). Africa predominantly uses 400×200×200mm and 450×225×225mm. Southeast Asia splits between 390×190×190mm and 400×200×200mm. Verify target market dimensions before specifying custom molds—non-standard sizes face acceptance challenges.
Climate and Mix Implications
High-strength mixes (≥25 MPa) require 10-15% more compaction force. In coastal or industrial environments using high-cement content, specify molds for machines with 15-20% force margin.
Dry-mix systems in water-scarce regions demand higher vibration intensity and longer cycles. Molds for diesel-powered machines in remote areas should emphasize durability over weight since replacement parts are distant.
Integration with Supporting Equipment
Pallet Compatibility
Molds must align with pallet dimensions and material. Wood pallets (850×550mm standard) accommodate most manual and semi-automatic molds. Steel pallets for automatic systems typically measure 1,050×680mm or 1,200×800mm. Plastic or composite pallets require mold designs ensuring complete block support during demolding—unsupported edges crack.
Verify pallet board thickness compatibility. Standard molds accommodate 15-20mm boards. Thicker boards (25-30mm, common in heavy-duty automatic systems) may require mold modifications to maintain proper core pin heights.
Conveyor System Coordination
Automated conveyor systems transport pallet boards with fresh blocks from machines to curing areas. Mold cavity spacing must align with downstream equipment—blocks positioned too close to edges risk damage. Maintain ≥40mm edge clearance for conveyor-compatible layouts.
Robotic stacking systems require precise block positioning within ±5mm tolerance. Molds for fully automated plants need tighter manufacturing tolerances than manual operations.
الأسئلة الشائعة
Can I use the same mold on different machine brands?
Potentially, if platform dimensions and mounting patterns match. Verify: 1) Mold dimensions fit within machine platform, 2) Mounting holes align with pallet guides, 3) Mold height allows proper clearance, 4) Machine pressing force adequate for cavity count. Many Chinese manufacturers use standardized dimensions allowing cross-compatibility, but European and specialized machines often require brand-specific molds.
How much does cavity count affect block quality?
Higher cavity counts require stronger vibration and compaction to achieve uniform density across all cavities. Machines operating near force capacity with maximum cavity molds produce 8-15% strength variation between center cavities (higher density) and edge cavities (lower density). Quality-critical applications should operate at 80-85% of maximum cavity capacity.
Should I buy multiple molds immediately or start with one?
Start with your primary product mold (typically standard hollow blocks) optimized for maximum efficiency. Operate 3-6 months establishing demand patterns before investing in additional molds. This approach conserves capital, provides real production data, allows market testing, and builds operator experience before complex designs.
What’s the real cost difference between 4-cavity and 6-cavity molds?
Initial cost: $400-$600 higher for 6-cavity (+30-35%). Lifetime cost per block: 6-cavity is 8-10% lower due to higher capacity spreading fixed costs. Break-even: 80,000-120,000 blocks. For operations exceeding 200,000 blocks annually, 6-cavity delivers superior economics despite higher upfront cost.
Can molds be modified after manufacturing?
Simple modifications—adjusting cavity depth, enlarging drain holes, adding mounting brackets—are straightforward. Complex changes—adding cavities, changing block geometry, relocating cores—often cost 50-70% of new mold price while compromising structural integrity. If requirements shift significantly, replacement is more economical than extensive modification.
How do I maintain dimensional accuracy?
Monthly measurement of critical dimensions using precision calipers. Track measurements identifying wear trends. Refurbish molds when dimensions drift beyond specification (±2-3mm for standard blocks, ±1mm for precision applications). Store molds properly—covered, elevated from ground, protected from moisture and impacts.
What causes premature mold failure?
Top three causes: 1) Inadequate cleaning allowing concrete buildup stressing metal during compaction (40% of failures), 2) Operating beyond design capacity—excessive force, wrong mix, improper vibration (30%), 3) Poor maintenance—ignored cracks, bent components, corrosion (20%). Proper daily cleaning and monthly inspection prevent 70-80% of premature failures.
Are Chinese-made molds comparable to European molds?
Quality spans wide ranges in both regions. Top-tier Chinese manufacturers using alloy steel and precision machining produce molds matching European specifications at 40-50% lower cost. However, budget Chinese molds using inferior steel and loose tolerances fail at 30,000-40,000 cycles versus 80,000-100,000+ for quality European molds. Specify material composition (45# or 40Cr steel minimum), manufacturing tolerances (±1mm), and request references from users in similar production volumes.
الخلاصة
Mold selection determines production capacity, block quality, and operational costs for 5-8 years. Choosing based solely on initial price leads to capacity constraints and costly mid-production replacements disrupting operations and customer commitments.
The optimal mold balances cavity count with machine capabilities, matches material durability to production volume, and accommodates your target market’s block specifications. For standard hollow block production exceeding 200,000 blocks annually, invest in 6-cavity alloy steel molds that reduce per-block costs 8-10% while providing 50% higher capacity than 4-cavity alternatives.
Whether operating manual systems, semi-automatic machines, or fully automatic plants, specify molds using this framework: match cavities to machine force and target output, select materials based on volume and environment, verify dimensional compatibility with standards and supporting equipment, and maintain according to schedules preventing 70-80% of premature failures.
Contact Raytone Block Machinery for custom mold design, cavity configuration recommendations, and technical specifications optimizing your block production system.