Block manufacturers evaluating production strategies in 2026 face a fundamental choice: fly ash blocks or conventional cement blocks. This comparison determines raw material costs, environmental compliance positioning, and profit margins as decarbonization mandates reshape construction procurement.
The global fly ash bricks market reached $4.07 billion in 2025 and projects 10.4% CAGR through 2033, while conventional cement block demand grows at 2.9% annually. Understanding material costs, strength performance, and manufacturing equipment reveals why this profitability gap exists.
Material Cost Analysis: The Profitability Driver
Cement Block Material Costs
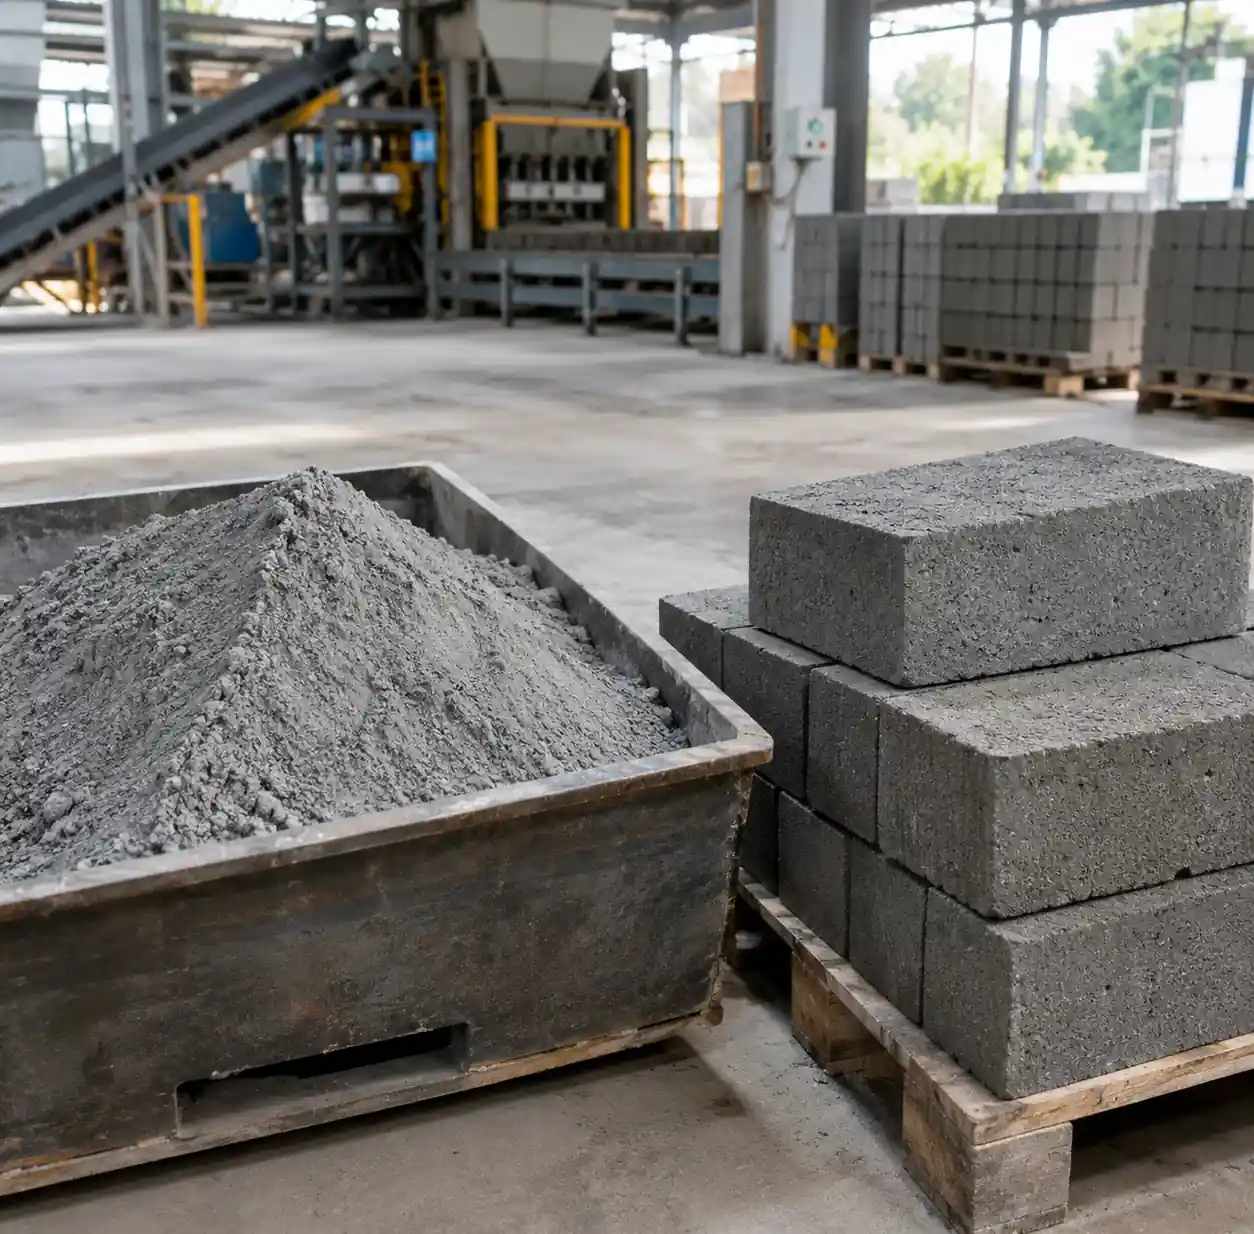
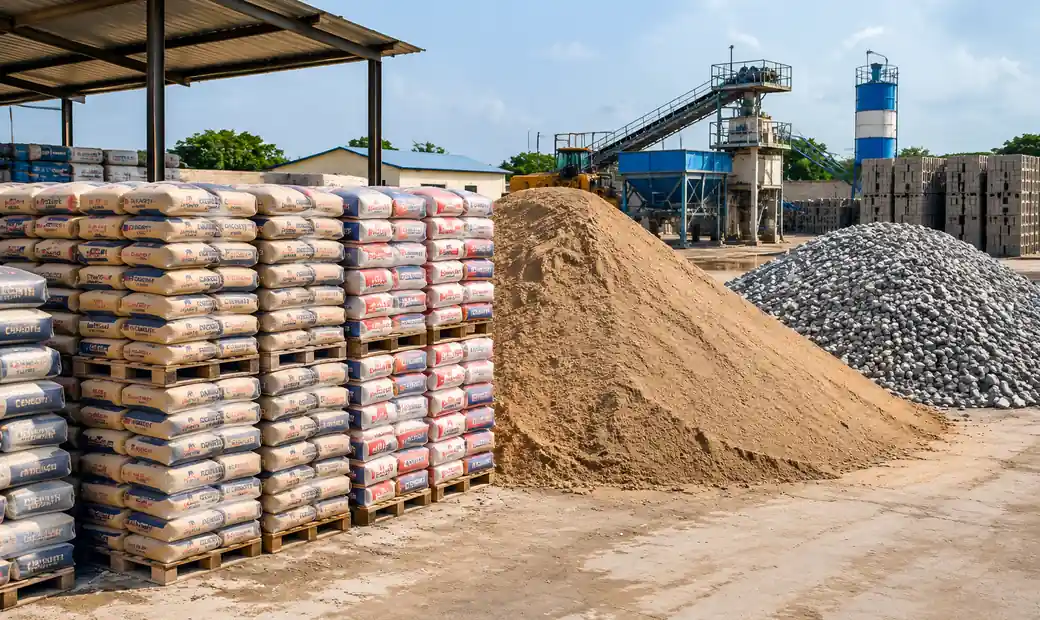
Conventional cement blocks use Portland cement (10-15% by weight) as the primary binder, combined with sand aggregates and water. Cement prices fluctuate between $95-140 per metric ton, making it the most expensive input in traditional block production.
A standard 400×200×200mm hollow cement block requires approximately 1.8-2.2 kg of cement. At $120/ton cement cost, the binder alone costs $0.22-0.26 per block before accounting for sand ($15-25/ton), water, and energy.
Fly Ash Block Material Costs
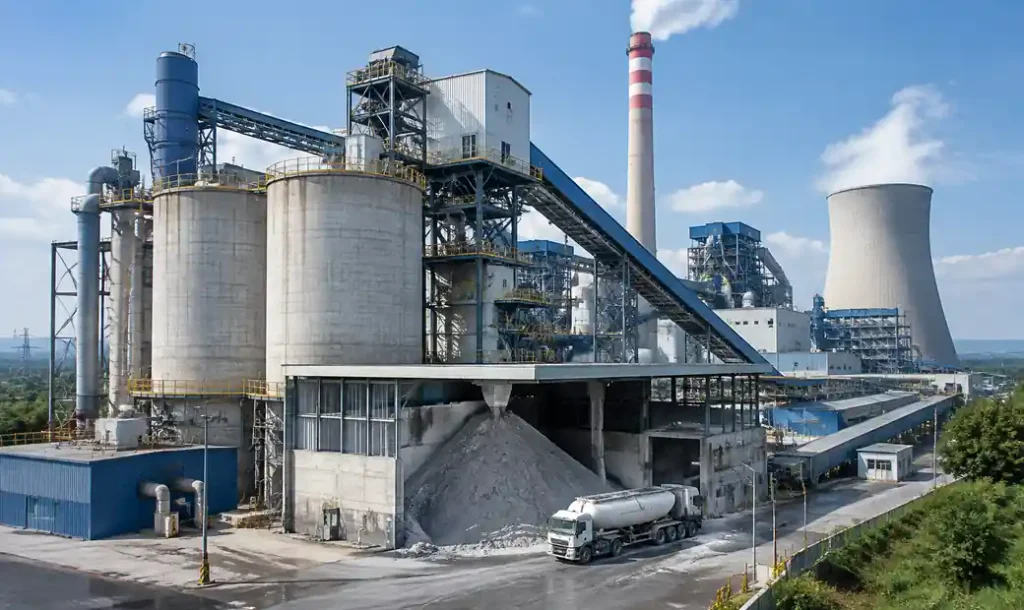
Fly ash blocks substitute 40-70% of Portland cement with fly ash, a coal combustion byproduct captured from thermal power plants. Fly ash costs $8-25 per ton—an 80-95% reduction compared to cement pricing.
A fly ash block using 60% fly ash replacement contains approximately 0.7-0.9 kg cement and 1.1-1.4 kg fly ash. Material cost breakdown: cement portion $0.08-0.11, fly ash portion $0.01-0.04, total binder cost $0.09-0.15 per block—a 40-60% reduction versus cement-only blocks.
Material Cost Comparison
| Material Input | Cement Blocks | Fly Ash Blocks (60% replacement) | Cost Savings |
|---|---|---|---|
| Cement (per block) | 1.8-2.2 kg @ $120/ton | 0.7-0.9 kg @ $120/ton | 61-59% less cement |
| Fly Ash (per block) | 0 kg | 1.1-1.4 kg @ $20/ton | $0.02-0.03 addition |
| Sand/Aggregates | 7-8 kg @ $20/ton | 7-8 kg @ $20/ton | No difference |
| Total Material Cost | $0.36-0.42 per block | $0.23-0.29 per block | 36-31% savings |
| Per 1,000 blocks | $360-420 | $230-290 | $130 savings |
At commercial scale (2,000 blocks daily), facilities save $260-320 per day, translating to $78,000-96,000 annually in material costs alone.
Production Equipment and Process
Equipment Requirements
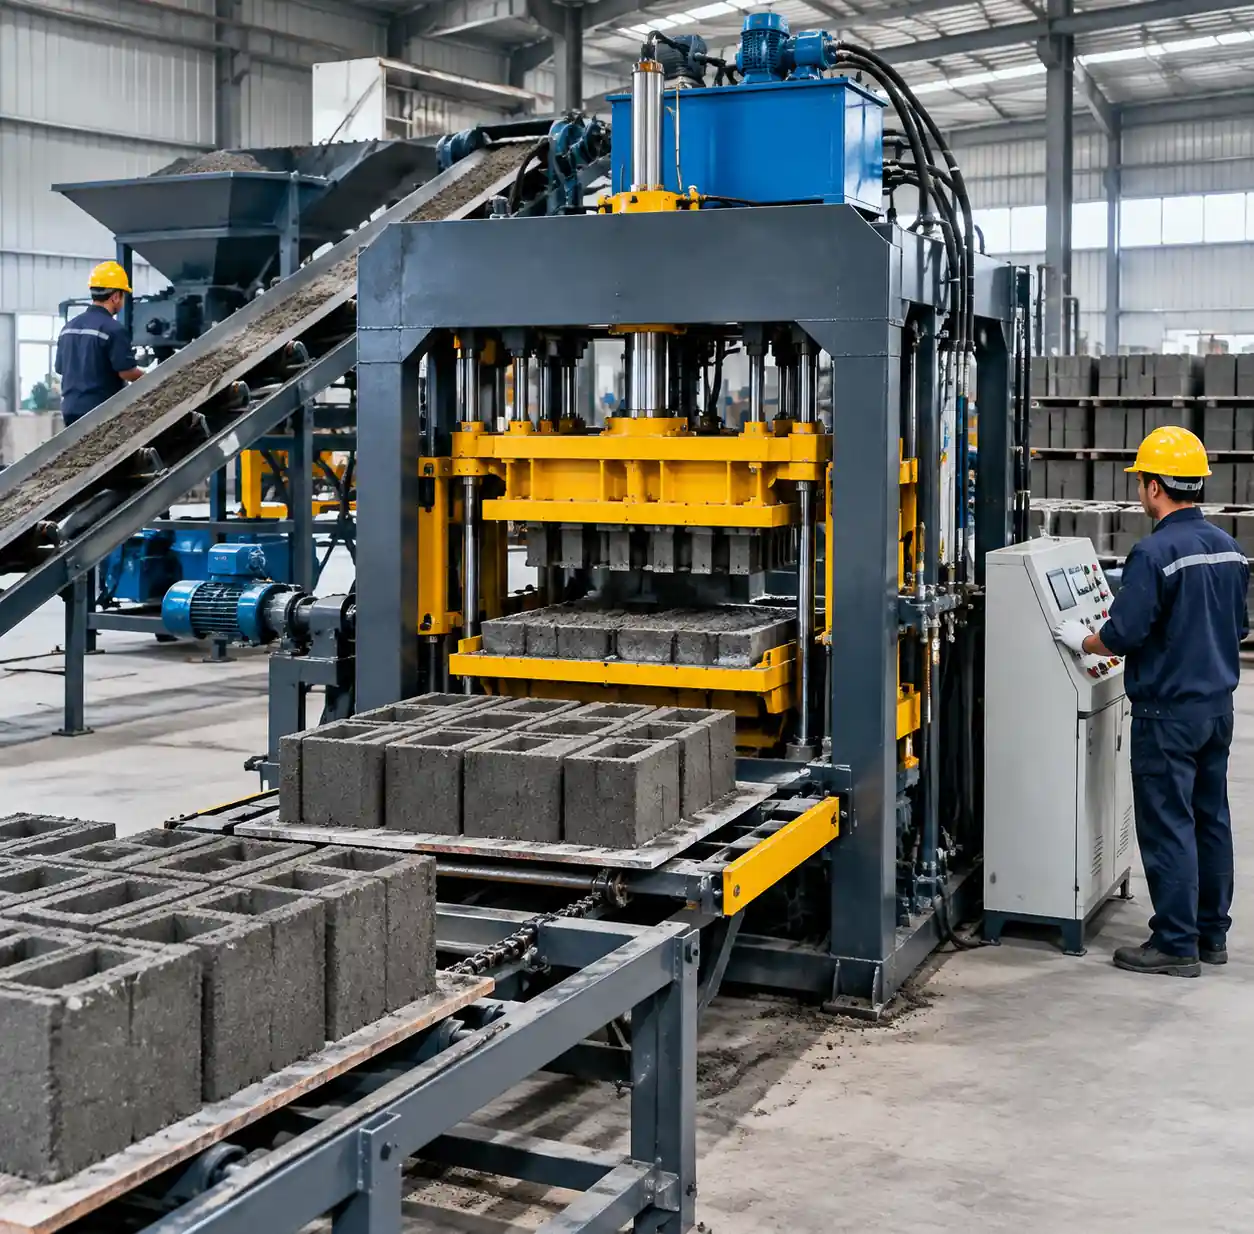
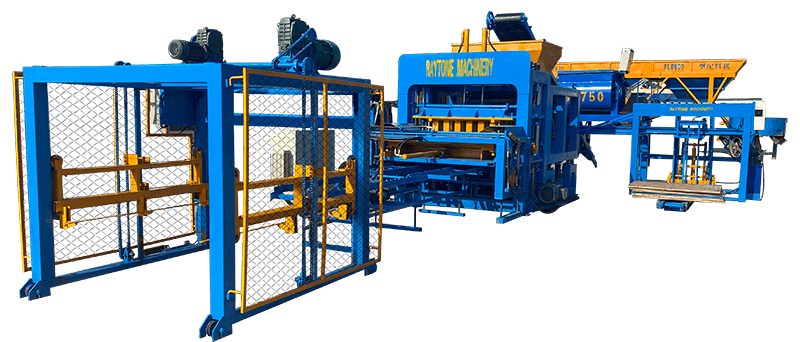
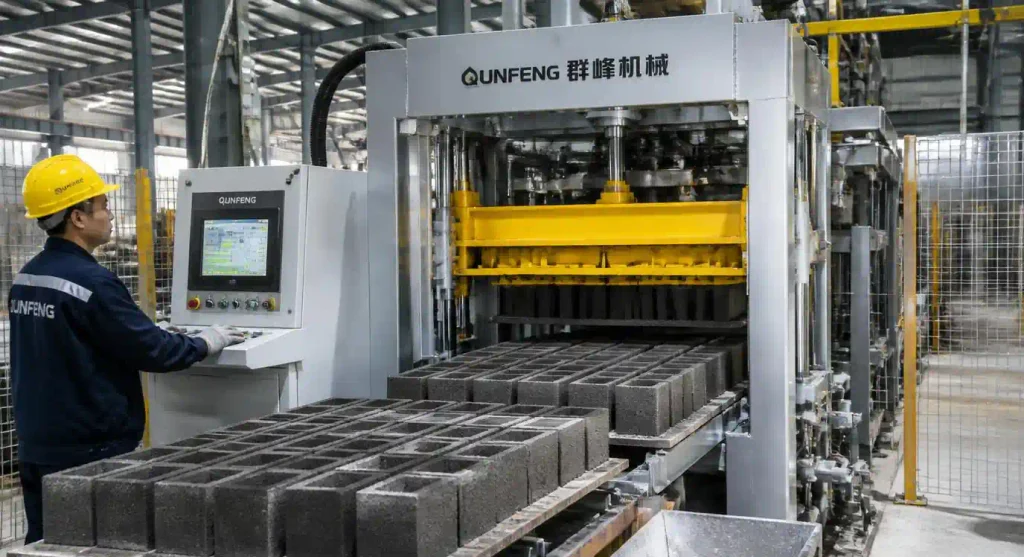
The same hydraulic block machines produce both cement and fly ash blocks with identical mold configurations. Semi-automatic models (QT4-40, producing 1,600-2,400 blocks/shift) cost $9,000-15,000, while fully automatic systems (QT8-15, producing 5,000+ blocks/shift) cost $28,000-35,000.
Process Advantages of Fly Ash
Fly ash blocks benefit from pozzolanic reactions—fly ash particles react with calcium hydroxide released during cement hydration, forming additional binding compounds. This reaction continues for weeks, delivering superior late-age strength.
Fly ash mixtures exhibit better workability due to spherical particle morphology, reducing mixer wear and allowing slightly lower water content (8-10% vs 10-12%). Production cycle times remain identical at 15-20 seconds per block for automatic machines. Fly ash blocks achieve 70-80% of final strength within 7 days versus 60-70% for cement blocks, enabling faster inventory turnover.
Strength Performance and Quality Standards
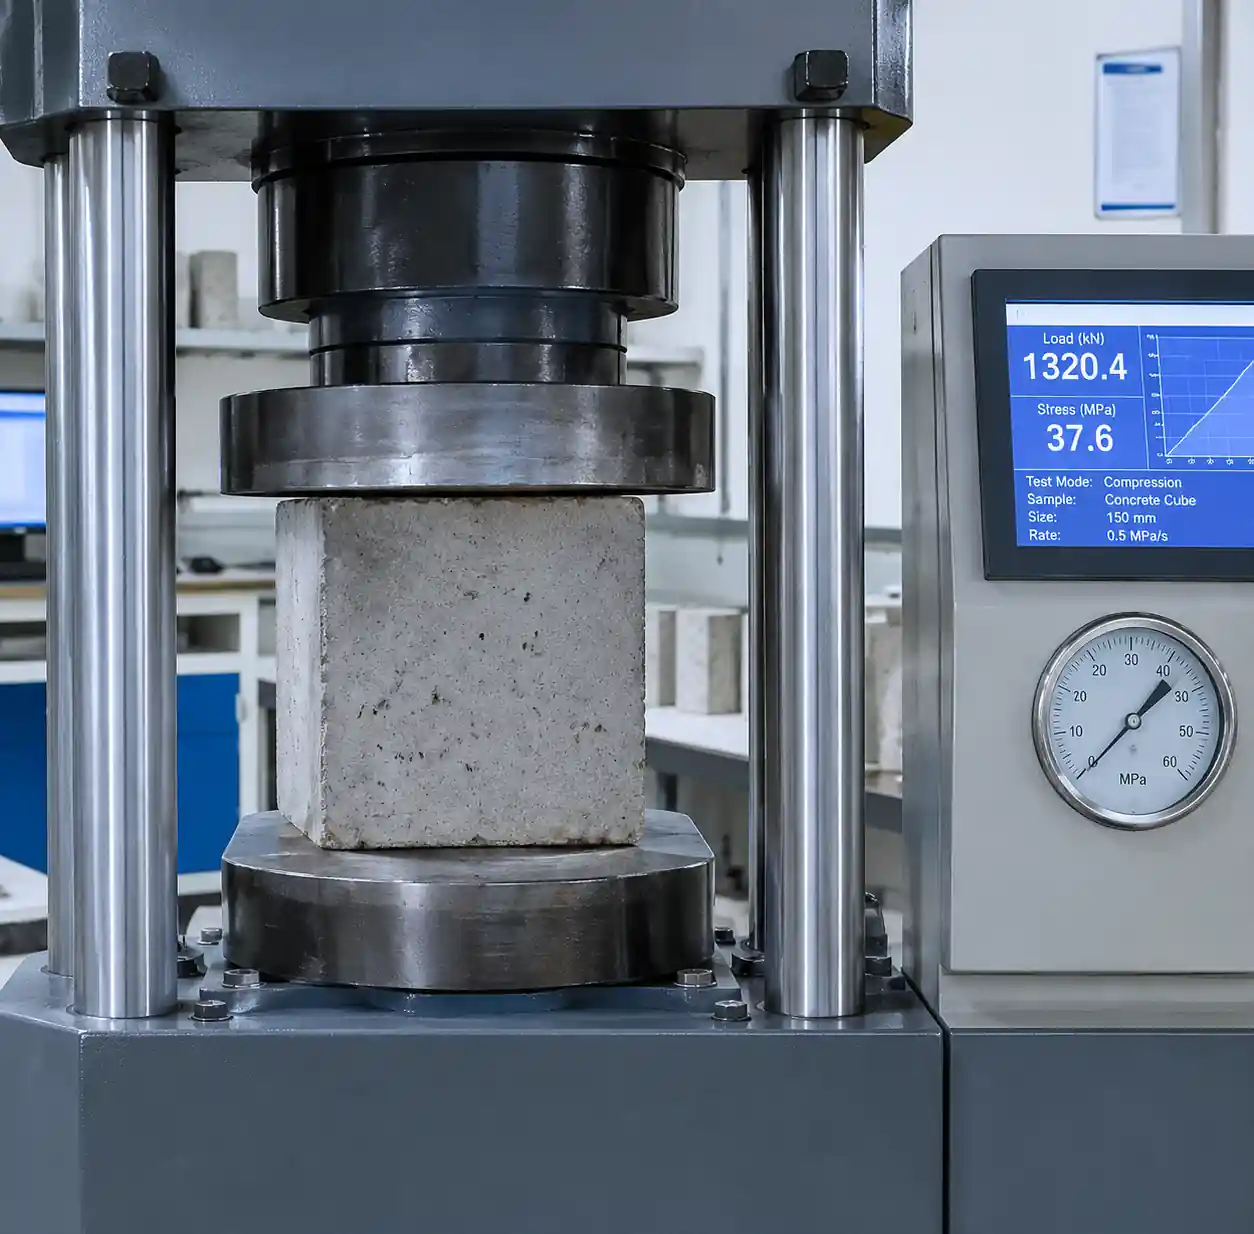
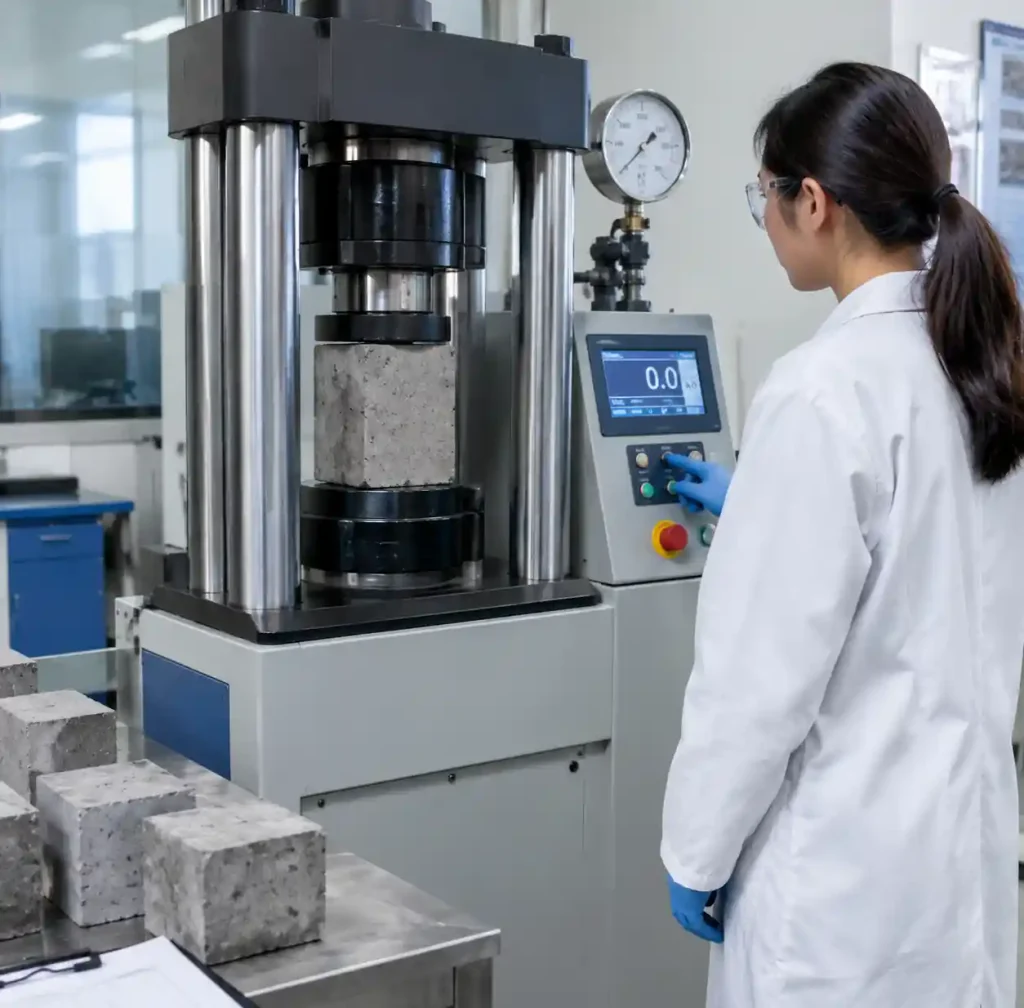
Research demonstrates fly ash blocks achieve comparable or superior strength to cement blocks. A 2025 MDPI sustainability study found optimal fly ash mixtures achieved 14.1% higher compressive strength and 15.3% higher flexural strength compared to pure cement mixes at 56 days.
Standard cement blocks achieve 4-7 MPa at 28 days. Fly ash blocks with 50-60% replacement reach 5-8 MPa at 28 days, with continued strength gain to 7-10 MPa by 90 days as pozzolanic reactions progress.
| Property | Cement Blocks | Fly Ash Blocks (50-60% replacement) |
|---|---|---|
| 28-day Compressive Strength | 4-7 MPa (580-1,015 psi) | 5-8 MPa (725-1,160 psi) |
| 90-day Compressive Strength | 5-8 MPa (725-1,160 psi) | 7-10 MPa (1,015-1,450 psi) |
| Water Absorption | 12-15% | 8-12% (improved) |
| Thermal Conductivity | 0.7-0.9 W/mK | 0.5-0.7 W/mK (better insulation) |
Fly ash blocks demonstrate superior sulfate resistance, reduced water permeability (15-25% improvement), and better alkali-silica reaction mitigation—key durability advantages for long-term performance.
Environmental Benefits and Market Positioning
Portland cement production generates approximately 0.8-0.9 kg CO₂ per kg cement. Fly ash blocks with 60% replacement reduce embodied carbon by 48-54% per block—a compelling advantage as construction procurement increasingly weighs carbon intensity.
Government infrastructure projects in Europe, California, and Singapore now mandate embodied carbon disclosure and often specify maximum carbon thresholds. Manufacturers producing fly ash blocks position themselves to capture specification-driven contracts that cement block producers cannot fulfill.
Thermal power plants generate 780 million tons of fly ash globally each year, with 60-70% historically requiring landfill disposal at $15-40 per ton. Block manufacturers transform this industrial waste stream into construction products, creating circular economy narratives valuable for LEED, BREEAM, and green building certifications.
Market Demand and Pricing Strategy
Current Market Growth
Le global fly ash market reached $14.9 billion in 2025, with fly ash bricks and blocks representing the fastest-growing application segment at 10.4% CAGR—significantly outpacing the 2.9% growth in conventional brick markets.
Asia-Pacific dominates with 75% market share, driven by rapid urbanization and infrastructure development. Government mandates in India require fly ash utilization in all construction projects within 100 km of thermal plants, creating guaranteed demand.
Profitability Analysis
Fly ash blocks typically sell at 5-15% discount to equivalent cement blocks despite lower production costs, creating the profitability advantage. Example economics for semi-automatic production (2,000 blocks/day, 300 operating days):
Cement Block Operation:
- Revenue: 600,000 blocks × $0.65 = $390,000
- Material costs: $234,000
- Labor (4 workers × $800/month × 12): $38,400
- Utilities and maintenance: $28,000
- Annual profit: $89,600
- Equipment payback: 20-24 months
Fly Ash Block Operation:
- Revenue: 600,000 blocks × $0.58 = $348,000
- Material costs: $156,000
- Labor (4 workers × $800/month × 12): $38,400
- Utilities and maintenance: $28,000
- Annual profit: $125,600
- Equipment payback: 14-17 months
The fly ash operation generates 40% higher annual profit ($36,000 additional) despite 11% lower selling prices. Over five-year equipment lifespan, cumulative additional profit reaches $180,000.
Automatic Production Profitability
Automatic block machines like QT8-15 cost $28,000-35,000 and produce 1.5 million blocks annually (300 days × 5,000 blocks).
Cement Block Operation:
- Revenue: 1,500,000 blocks × $0.63 = $945,000
- Material costs: $585,000
- Labor and utilities: $133,200
- Annual profit: $226,800
Fly Ash Block Operation:
- Revenue: 1,500,000 blocks × $0.56 = $840,000
- Material costs: $390,000
- Labor and utilities: $133,200
- Annual profit: $316,800
The automatic fly ash operation generates $90,000 additional annual profit—a 40% improvement that compounds to $450,000 over five years.
Regulatory Compliance and Key Challenges
Fly ash blocks meeting ASTM C90 (North America), BS 6073 (UK/Commonwealth), or IS 12894 (India) standards qualify for load-bearing and non-load-bearing applications identical to cement blocks. Initial testing costs $2,000-4,000 for complete certification, with annual surveillance audits at $800-1,200.
Supply consistency: Block producers depend on thermal power plant output schedules. Successful operations maintain 30-45 day fly ash inventory and establish contracts with multiple plants within 100 km radius.
Market perception: Architects and engineers unfamiliar with fly ash blocks may default to cement blocks in specifications. Technical marketing with test reports, case studies, and sample blocks overcomes this. Budget 5-10% of revenue for technical sales support during market entry.
Quality control: Fly ash composition varies between power plants. Producers must test each batch for loss on ignition (LOI), fineness, and chemical composition. High LOI (>6%) compromises strength. Quality control protocols add $8,000-15,000 to initial setup costs.
Equipment Selection Guide
Machines manuelles (QT4-40 Manual, $7,000-9,000): Suitable for 800-1,200 blocks/shift with 5-6 workers. Best for testing fly ash blocks before scaling production.
Machines semi-automatiques (QT4-40 Semi-Auto, $11,000-15,000): Produce 1,600-2,400 blocks/shift with 3-4 workers. Optimal for small to medium operations where material savings justify investment.
Automatic machines (QT8-15, $28,000-35,000): Produce 4,000-6,000 blocks/shift with 2-3 operators. Justify investment when production exceeds 1.5 million blocks annually and material cost savings ($195,000+ annual) accelerate ROI.
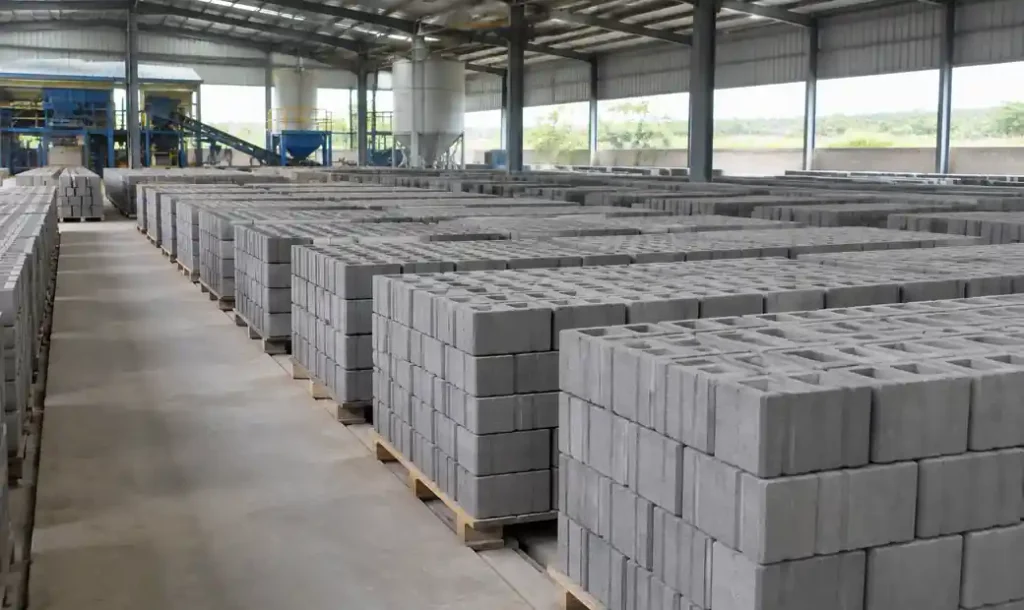
Raytone Block Machinery offers complete production solutions including mixers, conveyors, and curing systems compatible with both cement and fly ash formulations.
FAQ
How much cheaper are fly ash blocks to produce than cement blocks?
Material costs for fly ash blocks run 30-40% lower than cement blocks—typically $0.23-0.29 per block versus $0.36-0.42 for cement blocks. At commercial scale (2,000+ blocks daily), this translates to $78,000-96,000 annual material savings, achieving 35-45% higher profit margins.
Do fly ash blocks have the same strength as cement blocks?
Fly ash blocks with 50-60% cement replacement achieve 5-8 MPa compressive strength at 28 days, comparable to standard cement blocks at 4-7 MPa. Fly ash blocks gain additional strength through pozzolanic reactions, reaching 7-10 MPa by 90 days—often exceeding cement block final strength.
What equipment is needed to manufacture fly ash blocks?
The same hydraulic block machines produce both cement and fly ash blocks. Semi-automatic machines like QT4-40 ($11,000-15,000) suit small to medium operations, while automatic machines like QT8-15 ($28,000-35,000) serve high-volume production. Supporting equipment—pan mixer, conveyor system, and curing area—remains identical for both materials.
Is there reliable demand for fly ash blocks?
The global fly ash bricks market grew 10.4% annually through 2025, reaching $4.07 billion, driven by sustainability mandates and infrastructure development. Government specifications increasingly require or incentivize fly ash usage. Market growth significantly outpaces conventional cement block demand at 2.9% annually.
Where can I source fly ash for block production?
Contact regional coal-fired thermal power plants within 100 km to negotiate supply contracts. Fly ash costs $8-25 per ton, often with free or low-cost acquisition since plants otherwise pay disposal fees. Establish relationships with multiple suppliers to ensure consistent supply during plant maintenance periods.
How long does it take to recover equipment investment?
For semi-automatic production at 2,000 blocks daily, fly ash operations recover a $15,000-18,000 equipment investment in 14-17 months versus 20-24 months for cement operations. At automatic production scale (5,000 blocks daily), fly ash operations recover $30,000-35,000 investment in 11-13 months versus 15-18 months for cement blocks.
Conclusion
Fly ash blocks deliver 35-45% higher profit margins than cement blocks through 30-40% lower material costs while meeting equivalent strength standards. Market momentum favors fly ash blocks with 10.4% annual growth driven by decarbonization mandates.
For block producers, fly ash blocks offer $36,000-90,000 additional annual profit at small to medium scale, with faster equipment ROI and regulatory compliance advantages. The primary challenge—market education—diminishes as fly ash blocks gain mainstream acceptance.
Raytone Block Machinery provides hydraulic block machines et complete production solutions optimized for both cement and fly ash manufacturing.